
Views: 276 Author: 广宇大 Publish Time: 2026-11-06 Origin: Site


Content Menu
● What Are Water-Based Coatings?
>> Definition and Core Function
● What Are Solvent-Based Coatings?
>> Definition and Core Function
● Water-Based vs Solvent-Based: The Core Difference
>> How Water-Based Coatings Work in Linear Spraying
>> How Solvent-Based Coatings Work in Linear Spraying
● Film Build, Transfer Efficiency, and Coating Consumption
● Drying, Curing, and Line Balancing
>> Solvent-Based Coating Drying
● Equipment Compatibility and Maintenance
>> Water-Based Coating Equipment
>> Solvent-Based Coating Equipment
● Safety, Ventilation, and Fire Prevention
● A Practical Selection Framework
>> Choose Water-Based Coatings When:
>> Choose Solvent-Based Coatings When:
>> Consider a Hybrid Approach When:
● A Practical Validation Roadmap
>> Step 1: Define the Product Family
>> Step 2: Run a Coating Trial
>> Step 3: Validate the Complete Line
>> Step 4: Train Operators and Technicians
>> Step 5: Standardize Recipes and Maintenance
● Common Problems and Expert Solutions
>> Overspray and Filter Loading
>> Color Variation Between Batches
>> Daily Checks
● How GYDFinishing Approaches Coating Selection
>> What is the main difference between water-based and solvent-based coatings?
>> Which coating is better for automatic linear profile spraying?
>> Do water-based coatings still require a spray booth?
>> Which coating produces less overspray?
>> How should I compare production speed?
>> Can a line use both water-based and solvent-based coatings?
Choosing between water-based coatings and solvent-based coatings for automatic linear profile spraying depends on profile geometry, drying method, target film build, environmental requirements, production volume, and total cost of ownership. Water-based coatings are often easier to clean and may support lower-VOC strategies. Solvent-based coatings can offer fast flash-off and strong flow in some formulations, but require stricter ventilation, ignition-source control, and solvent-compatible equipment.
From an equipment manufacturer's perspective, the coating should not be selected in isolation. For wooden doors, cabinet doors, mouldings, furniture components, and flooring profiles, the best choice depends on substrate, viscosity, transfer efficiency, drying or curing method, booth airflow, operator safety, coating consumption, and accepted finished parts per shift.
This guide compares both coating systems from a practical production standpoint. It explains how each works, where each performs best, and how to validate the right solution for your automatic linear profile spraying line.
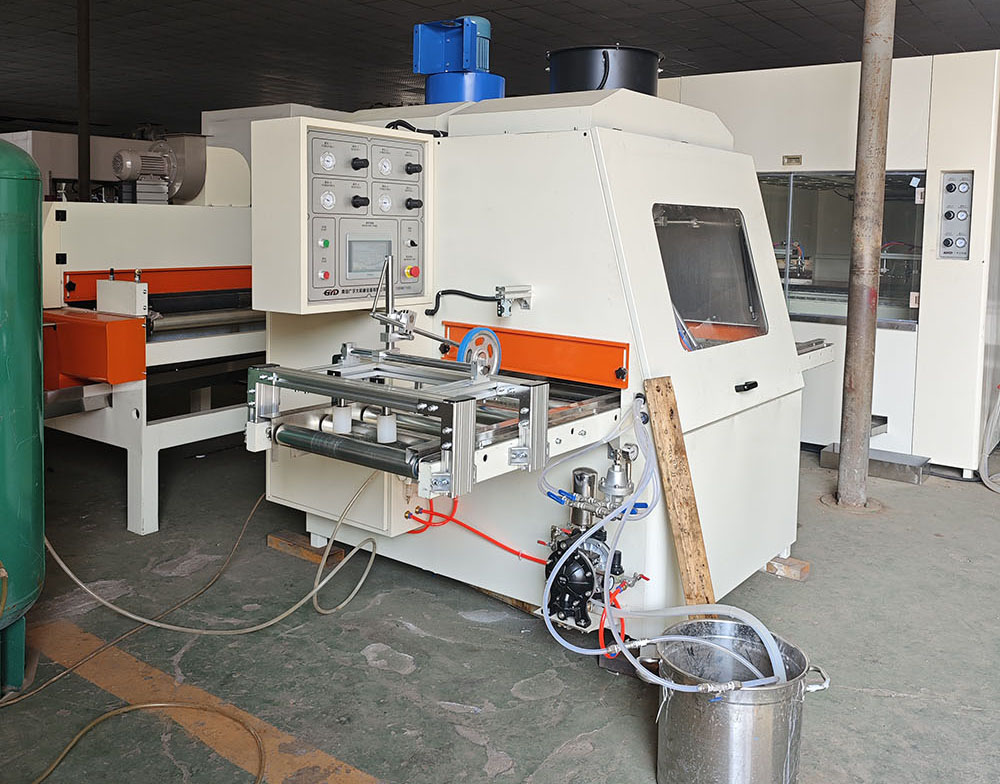
Water-based coatings use water as the primary carrier or diluent. They may include acrylic, polyurethane, hybrid, or other resin systems.
In automatic linear profile spraying, water-based coatings are applied through pumps, hoses, filters, spray guns, and drying equipment designed for water-based materials.
Key point: "Water-based" does not mean "no ventilation required." The need for ventilation depends on the hazardous chemicals present in the coating, not simply whether the carrier is water. [1805]
Water-based coatings are commonly used for:
- Wooden doors and cabinet doors
- Mouldings and decorative trim
- Furniture rails and panels
- Flooring profiles and skirting
- Primer, sealer, stain, and topcoat application
- Production lines with environmental or VOC-reduction goals
- Factories seeking easier cleanup
They are most effective when the drying system, coating formulation, and equipment are properly matched.
Solvent-based coatings use organic solvents as the primary carrier or diluent. They may include lacquers, polyurethanes, alkyds, or other resin systems.
In automatic linear profile spraying, solvent-based coatings are applied through pumps, hoses, filters, spray guns, and drying equipment designed for solvent-based materials.
Key point: Solvent-based coatings can offer fast flash-off and strong flow in some formulations, but they introduce greater fire, explosion, and ventilation requirements.
Solvent-based coatings are commonly used for:
- Wooden doors and cabinet doors
- Mouldings and decorative trim
- Furniture rails and panels
- Flooring profiles and skirting
- High-gloss or fast-drying finishes
- Production lines with solvent-compatible equipment
- Applications where specific coating performance is required
They are most effective when the booth, ventilation, electrical classification, and coating formulation are properly matched.
The fundamental difference is the carrier and drying behavior.
- Water-based coatings use water as the main carrier and typically require controlled temperature and airflow for drying.
- Solvent-based coatings use organic solvents and may flash off faster, but they require stricter ventilation and ignition-source control.
Both systems can be automated. Both can produce high-quality finishes. The better choice depends on the substrate, coating, and production objective.
A typical water-based coating process follows this flow:
1. Prepare the water-based coating to the specified viscosity.
2. Load the profile onto the conveyor.
3. Detect the part and select the coating recipe.
4. Move the profile through the spray zone.
5. Activate the spray guns only when a part is present.
6. Apply coating using controlled gun settings and line speed.
7. Capture overspray through the booth exhaust and filters.
8. Send the coated profile to flash-off, drying, or curing.
9. Clean the system with water-based cleaning procedures.
The most important variables are coating viscosity, line speed, gun distance, spray angle, fluid output, atomizing air, booth temperature, airflow, and drying time.
A typical solvent-based coating process follows this flow:
1. Prepare the solvent-based coating to the specified viscosity.
2. Load the profile onto the conveyor.
3. Detect the part and select the coating recipe.
4. Move the profile through the spray zone.
5. Activate the spray guns only when a part is present.
6. Apply coating using controlled gun settings and line speed.
7. Capture overspray through the booth exhaust and filters.
8. Send the coated profile to flash-off, drying, or curing.
9. Clean the system with solvent-compatible cleaning procedures.
The most important variables are coating viscosity, solvent balance, line speed, gun distance, spray angle, fluid output, atomizing air, booth airflow, and drying time.
Film build is the thickness of coating applied to the profile. It affects appearance, durability, drying time, and downstream sanding.
For both coating types, film build is influenced by:
- Coating viscosity
- Fluid output
- Number of spray passes
- Gun distance
- Spray angle
- Line speed
- Atomizing air
- Fan air
The correct approach is to establish a validated process window: a range of settings that consistently produces acceptable results.
Transfer efficiency is the percentage of coating that actually reaches the workpiece. Higher transfer efficiency reduces material waste, booth contamination, and filter loading.
Water-based coatings can achieve high transfer efficiency when gun distance, fan pattern, and atomizing air are optimized. Solvent-based coatings can also achieve high transfer efficiency, but results depend more on solvent balance, viscosity, and booth airflow.
Expert insight: The lowest-cost coating is not always the one with the lowest price per liter. A coating that wastes less material, produces fewer rejects, and requires less cleaning may deliver a lower total cost of ownership.
Water-based coatings often require controlled temperature and airflow during drying.
Key drying variables include:
- Booth temperature
- Relative humidity
- Airflow direction
- Air velocity
- Flash-off time
- Coating thickness
- Substrate temperature
A fast spray station cannot compensate for a slow drying stage. The complete line must be balanced:
Spray → flash-off → dry → sand if required → second coat if required → final inspection.
Solvent-based coatings may flash off faster depending on the formulation.
Key drying variables include:
- Solvent evaporation rate
- Booth temperature
- Airflow direction
- Air velocity
- Flash-off time
- Coating thickness
- Substrate temperature
Solvent-based coatings may require stricter ventilation and ignition-source control because solvent vapors can create fire and explosion hazards. OSHA notes that spray painting releases flammable and combustible vapors, increasing the potential for fires or explosions. [2301]
Water-based coatings require equipment that resists corrosion and handles water-based cleaning.
Key equipment considerations include:
- Stainless or compatible pump components
- Water-resistant hoses and seals
- Compatible filters
- Suitable spray guns and nozzles
- Controlled drying temperature and humidity
- Water-based cleaning procedures
Water-based systems are often easier to clean, but they still require disciplined maintenance.
Solvent-based coatings require equipment that resists solvent attack and supports safe solvent handling.
Key equipment considerations include:
- Solvent-compatible pump components
- Solvent-resistant hoses and seals
- Compatible filters
- Suitable spray guns and nozzles
- Explosion-proof or appropriately classified electrical components where required
- Solvent-based cleaning procedures
Solvent-based systems may require more rigorous maintenance because solvent exposure can affect seals, hoses, and coatings on machine surfaces.
Spray finishing can release mists, vapors, and residues. OSHA identifies spray finishing using flammable and combustible materials as a regulated operation under 29 CFR 1910.107. [2330]
A spray booth is a power-ventilated structure provided to enclose or accommodate a spraying operation, confine and limit the escape of spray, vapor, and residue, and safely direct them to an exhaust system. [1720]
OSHA requires adequate local exhaust ventilation for coating and gluing processes, including manual spray, rolling, brushing, automated coating, and dip coating. [2331]
Ventilation must remain in operation during spraying and for a sufficient time afterward to allow vapors from drying coated articles and finishing-material residue to be exhausted. [1720]
OSHA also states that the total air volume exhausted through a spray booth should dilute solvent vapor to at least 25 percent of the lower explosive limit of the solvent being sprayed. [2202]
Both water-based and solvent-based systems should include:
- Properly designed spray booth or enclosed spray zone
- Mechanical exhaust ventilation
- Make-up air supply
- Filter maintenance program
- Grounding and bonding for static control
- Appropriate electrical classification where required
- Coating storage and handling controls
- Operator training
- Emergency stop and interlock systems
- Regular inspection of hoses, pumps, guns, and filters
Do not treat ventilation as an optional accessory. It is a core safety and quality system.
- You want easier cleanup and lower solvent handling.
- You have a drying system matched to water-based coatings.
- You are targeting lower-VOC or environmentally conscious production.
- Your profiles are suitable for water-based adhesion and drying.
- Your operators are trained in water-based coating control.
- You need fast flash-off or specific coating performance.
- You have a solvent-compatible spray system and booth.
- You can manage solvent storage, ventilation, and ignition-source control.
- Your profiles require a specific solvent-based finish.
- Your operators are trained in solvent-based coating control.
- You produce both standard and special finishes.
- You need high throughput for one coating type and flexibility for another.
- You want to separate primer and topcoat supply.
- You want to reduce cleaning between coating types.
A hybrid solution may use water-based coatings for standard production and solvent-based coatings for special finishes, provided the equipment and safety systems support both.
Document the profiles, dimensions, materials, coatings, target output, and quality standard.
Include photographs, drawings, and physical samples of the most difficult profile.
Test the actual profile with the intended coating. Record:
- Coating viscosity
- Gun distance
- Spray angle
- Fluid output
- Atomizing air
- Fan air
- Line speed
- Number of passes
- Film thickness
- Drying result
- Visual appearance
Do not judge only the spray station. Validate the complete sequence:
Coating → flash-off → cure → sanding if required → second coat if required → final inspection.
Operators should understand daily checks, coating preparation, part loading, and quality inspection. Technicians should understand gun setup, nozzle care, filters, pumps, electrical controls, and safety systems.
Create written recipes for each product family. Include coating type, viscosity, gun settings, line speed, curing conditions, and inspection criteria.
Schedule maintenance for filters, nozzles, pumps, hoses, conveyors, sensors, and ventilation equipment.
Likely causes:
- Incorrect gun distance
- Wrong spray angle
- Excessive line speed
- Insufficient gun coverage
- Profile movement or vibration
- Incorrect coating viscosity
- Poor booth airflow
Solution: Start with the most difficult profile. Adjust one variable at a time and record the result.
Likely causes:
- Excessive fluid output
- Incorrect fan pattern
- Gun too far from the part
- Poor gun activation timing
- Worn nozzles
- Excessive booth airflow
Solution: Optimize transfer efficiency before increasing exhaust capacity. A well-tuned spray process reduces booth contamination and filter replacement frequency.
Likely causes:
- Excessive atomizing air
- Incorrect solvent balance
- Gun too far from the workpiece
- Excessive booth airflow
- Incorrect coating temperature
Solution: Review the coating technical data and validate the spray distance, air settings, and booth environment.
Likely causes:
- Excessive film build
- Slow line speed
- Incorrect coating viscosity
- Insufficient flash-off time
- Poor gun overlap
Solution: Reduce film build or adjust line speed and flash-off conditions. Confirm that the coating is within its recommended application range.
Likely causes:
- Inconsistent coating mixing
- Changes in viscosity
- Different gun settings
- Inconsistent substrate color
- Inadequate cleaning between color changes
Solution: Standardize mixing, viscosity checks, gun recipes, and cleaning procedures.
- Inspect spray guns and nozzles.
- Check fluid hoses and connections.
- Confirm conveyor alignment.
- Verify booth airflow and filter condition.
- Inspect pumps, valves, and fluid lines.
- Check for leaks, air bubbles, or pressure fluctuation.
- Clean gun tips according to the coating manufacturer's instructions.
- Inspect emergency stops and safety interlocks.
- Check belt tension and conveyor tracking.
- Inspect gun carriage movement.
- Clean or replace filters as required.
- Check pump performance and fluid delivery.
- Review coating consumption and reject rates.
- Inspect ventilation fans and ducts.
- Check electrical connections and control panels.
- Review PLC alarms and error history.
- Calibrate sensors and verify safety devices.
- Audit recipes against actual production results.
GYDFinishing has manufactured surface finishing equipment since 2007 and provides solutions for wood, glass, fibre cement, and other materials. Its experience includes automatic coating equipment for wooden doors, furniture, cabinet doors, and flooring.
For a buyer comparing water-based coatings with solvent-based coatings, the most useful supplier discussion is not simply about coating type. It should focus on:
- The exact profile drawings and physical samples
- Coating type and target film thickness
- Required production output
- Available factory space and utilities
- Curing method and drying time
- Color-change frequency
- Operator skill level
- Maintenance and spare-part strategy
- Total cost of ownership
A credible supplier should be willing to test the customer's actual profiles and coating system, document the results, and explain the limitations as well as the benefits.
Water-based coatings use water as the main carrier and typically require controlled drying. Solvent-based coatings use organic solvents and may flash off faster but require stricter ventilation and ignition-source control.
It depends on the profile, drying system, and production goal. Water-based coatings suit lines with controlled drying and easier cleanup. Solvent-based coatings suit lines with solvent-compatible equipment and specific performance needs.
Yes, if hazardous chemicals are present. OSHA notes that the need for spray booth ventilation depends on the presence of hazardous chemicals in the coating, not simply whether the coating is water-based. [1805]
Neither coating automatically produces less overspray. Overspray depends on gun distance, fan pattern, fluid output, spray overlap, gun activation, and profile geometry. Both coatings must be validated with actual production parts.
Compare accepted finished parts per shift, not conveyor speed or drying time alone. Include loading, coating changes, cleaning, curing, inspection, rework, and downtime.
Yes, but only if the equipment, safety systems, and cleaning procedures support both. Many factories separate the two coating types to avoid contamination and simplify maintenance.
If you are deciding between water-based and solvent-based coatings for automatic linear profile spraying, start with a coating-specific finishing trial rather than a generic equipment quotation.
Send GYDFinishing your profile drawings, coating specification, target output, and factory layout. A practical evaluation should identify the right coating system, gun setup, drying method, and total line layout for your product family.
- After the introduction: AI image prompt: *Side-by-side industrial comparison of water-based and solvent-based coating systems on an automatic linear profile spraying line, clean modern factory, realistic photography, wide angle.*
- In the "How Each Coating Works" section: AI image prompt: *Cutaway technical illustration comparing water-based and solvent-based coating flow through pumps, hoses, spray guns, and drying zones, clean engineering illustration.*
- In the "Drying and Curing" section: AI image prompt: *Factory workflow illustration showing spray application, flash-off, drying, curing, inspection, and packaging for wooden profiles, no text.*
- In the "Safety" section: AI image prompt: *Technical illustration of spray booth airflow, intake air, exhaust duct, filters, grounding, and wooden profiles moving through the booth.*
- In the "Validation Roadmap" section: AI image prompt: *Flowchart-style factory illustration showing profile loading, coating application, flash-off, curing, inspection, and packaging.*
- OSHA, *29 CFR 1910.107 – Spray finishing using flammable and combustible materials*: [https://www.osha.gov/laws-regs/regulations/standardnumber/1910/1910.107]
- OSHA, *29 CFR 1910.94 – Ventilation*: [https://www.osha.gov/laws-regs/regulations/standardnumber/1910/1910.94]
- OSHA, *Chemical and Other Hazards in Painting*: [https://www.osha.gov/sites/default/files/2019-04/Chemicals_in_Painting_Materials.pdf]
- OSHA, *Hazard Communication in the Maritime Industry*: [https://www.osha.gov/sites/default/files/publications/OSHA3694.pdf]
- OSHA, *eTool: Sawmills – Plant-Wide Hazards*: [https://www.osha.gov/etools/sawmills/plant-wide-hazards/health-hazards/chemicals]
- OSHA, *Spray Operations – Overview*: [https://www.osha.gov/spray-operations]
- OSHA, *Spray Operations – Controlling Hazards*: [https://www.osha.gov/spray-operations/controlling-hazards]
- OSHA, *Requirements for spray booth when spraying water-based paint*: [https://www.osha.gov/laws-regs/standardinterpretations/2008-03-28]
- GYDFinishing company background supplied by the client.


