
Views: 259 Author: 广宇大 Publish Time: 2026-11-04 Origin: Site


Content Menu
● What Is a Single-Circuit Spray System?
>> Definition and Core Function
● What Is a Dual-Circuit Spray System?
>> Definition and Core Function
● Single-Circuit vs Dual-Circuit: The Core Difference
>> How a Single-Circuit System Works
>> How a Dual-Circuit System Works
● Color-Change Downtime and Material Waste
>> Why Color Changes Are Costly
>> Single-Circuit System Impact
● A Practical Color-Change Cost Framework
>> Step 1: Count Actual Color Changes
>> Step 2: Measure Current Changeover Time
>> Step 3: Calculate Coating and Cleaning Loss
>> Step 4: Compare Against Dual-Circuit Operation
>> Step 5: Calculate Total Cost of Ownership
● Film Build, Color Consistency, and Quality Control
>> Common Color-Change Defects
● Coating Types and Circuit Compatibility
>> Water-Based and Solvent-Based Coatings
● Ventilation, Safety, and Fire Prevention
>> Why Spray Booths Are Essential
● A Practical Selection Framework
>> Choose a Single-Circuit System When:
>> Choose a Dual-Circuit System When:
>> Consider a Multi-Circuit or Modular System When:
● A Practical Validation Roadmap
>> Step 1: Define the Color-Change Pattern
>> Step 2: Run a Coating Trial
>> Step 3: Validate the Complete Line
>> Step 4: Train Operators and Technicians
>> Step 5: Standardize Recipes and Maintenance
● Common Problems and Expert Solutions
>> Color Contamination After Changeover
>> Pressure or Flow Instability
>> Downtime During Color Changes
>> Daily Checks
● How GYDFinishing Approaches Color-Change Efficiency
>> What is the main difference between a single-circuit and dual-circuit spray system?
>> Which system is better for frequent color changes?
>> Can both systems apply water-based coatings?
>> Does a dual-circuit system eliminate cleaning?
>> How should I calculate the value of a dual-circuit system?
>> Can a spray system use more than two circuits?
Choosing between a single-circuit spray system and a dual-circuit spray system for frequent color changes comes down to downtime, coating waste, cleaning complexity, and production flexibility. A single-circuit system uses one coating supply path and must be flushed and refilled for every color change. A dual-circuit system maintains two separate coating paths, allowing faster switching between two colors or coating types.
From an equipment manufacturer's perspective, the right choice is not simply "more circuits equals better." For wooden doors, cabinet doors, mouldings, furniture components, and flooring products, the decision should be based on color-change frequency, batch size, coating type, cleaning time, material loss, operator skill, and total cost of ownership.
This guide compares both systems from a practical production standpoint. It explains how each works, where each performs best, and how to validate the best configuration for your actual color-change workflow.
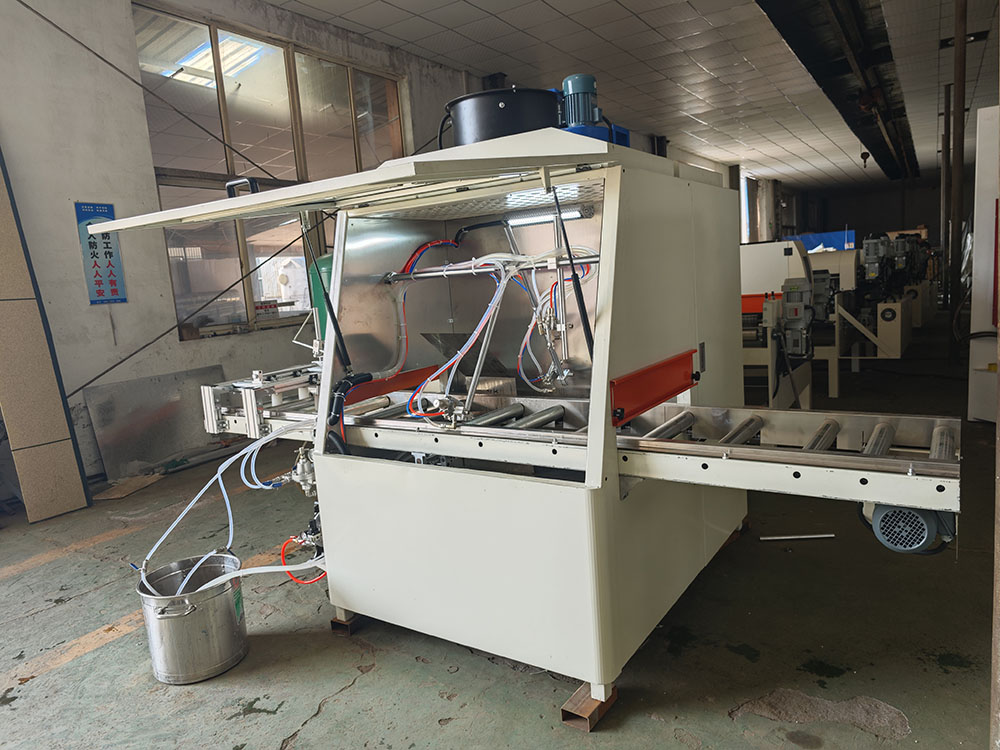
A single-circuit spray system uses one coating supply line, pump, filter, hose set, and spray-gun circuit. All colors are applied through the same fluid path.
When the production schedule changes color, the operator must stop the line, flush the circuit, clean or replace components where required, refill with the next coating, and verify that the new color is stable.
Key point: A single-circuit system is simple, compact, and cost-efficient. Its main trade-off is that every color change consumes time and coating material.
Single-circuit spray systems are commonly used for:
- Long production runs of one color
- Wooden door and cabinet-door finishing
- Furniture panels and mouldings
- Flooring products with limited color variation
- Primer or sealer application
- Factories with predictable production schedules
- Operations where coating waste and cleaning time are acceptable
They are most effective when color changes are infrequent and each batch is large enough to justify flushing and refilling.
A dual-circuit spray system uses two independent coating supply paths. Each path may include its own pump, fluid lines, filters, valves, and spray-gun circuit.
The system can switch between two coatings or colors without fully flushing the entire machine. For example, one circuit may supply white primer while the other supplies a tinted sealer, stain, or topcoat.
Key point: A dual-circuit system reduces color-change downtime when production regularly alternates between two colors or coatings. It also increases equipment complexity and cleaning requirements.
Dual-circuit spray systems are commonly used for:
- Frequent two-color production
- Door and cabinet-door factories
- Furniture lines with multiple finishes
- Moulding and trim production
- Flooring lines with alternating colors
- Primer and topcoat separation
- Water-based and solvent-based coating separation
- Production schedules with short batches
They are most effective when the product mix consistently uses two colors, two coatings, or two viscosity ranges.
The fundamental difference is how coating is delivered during color changes.
- In a single-circuit system, one fluid path serves all colors. Each change requires flushing, cleaning, and refilling.
- In a dual-circuit system, two fluid paths are available. The operator can switch between circuits instead of flushing the complete system.
Both systems can be automated. Both can deliver high-quality finishes. The better choice depends on the color-change pattern and production objective.
A typical single-circuit color-change process follows this flow:
1. Finish the current color batch.
2. Stop or slow the line.
3. Flush the pump, hoses, filters, and spray guns.
4. Clean or replace components as required.
5. Refill the coating supply system.
6. Prime the circuit with the new coating.
7. Run a test piece or purge material.
8. Verify color, viscosity, spray pattern, and film build.
9. Restart production.
The most important variables are flushing time, solvent or water consumption, coating loss, filter condition, pump condition, hose length, and operator procedure.
A typical dual-circuit color-change process follows this flow:
1. Finish the current color batch on Circuit A.
2. Switch the control system to Circuit B.
3. Activate the spray guns connected to Circuit B.
4. Run a short purge or test piece if required.
5. Verify color, viscosity, spray pattern, and film build.
6. Restart production.
7. Clean Circuit A later, during a planned pause or at the end of the shift.
The most important variables are circuit isolation, valve reliability, hose length, pump condition, cleaning schedule, and coating compatibility.
Color changes affect more than machine time. They can create:
- Lost production time
- Coating waste during flushing
- Solvent or water consumption
- Filter replacement
- Cleaning labor
- Color-contamination risk
- Test-piece waste
- Quality-control delays
A color change that takes only 15 minutes can become expensive when it occurs many times per shift.
A single-circuit system can be efficient for long runs. However, frequent color changes increase:
- Total flushing time
- Coating waste
- Solvent or water use
- Labor requirements
- Filter loading
- Risk of color contamination
The practical question is not whether the machine can change color. It is whether the number of color changes per shift makes the downtime acceptable.
A dual-circuit system can reduce downtime when production alternates between two established colors or coatings.
It can reduce:
- Full-system flushing frequency
- Waiting time between colors
- Coating waste during routine changes
- Operator intervention
- Production interruptions
However, both circuits still require cleaning. A dual-circuit system does not eliminate maintenance; it redistributes it.
Expert insight: The best system is the one that matches your actual color-change pattern. A dual-circuit system may be unnecessary if your factory changes color only once per day, but it can deliver major gains if you alternate colors several times per shift.
Record the number of color changes per shift, per day, and per week.
Include:
- Planned color changes
- Unplanned color changes
- Coating changes
- Viscosity changes
- Primer-to-topcoat changes
Time the complete process from the last acceptable part of the old color to the first acceptable part of the new color.
Include:
- Line stop
- Flushing
- Cleaning
- Refilling
- Priming
- Testing
- Quality approval
- Restart
Record:
- Coating volume lost during flushing
- Solvent or water used
- Filter changes
- Cleaning cloths or consumables
- Labor time
- Test-piece waste
Run a trial with a dual-circuit system using your two most frequent colors or coatings.
Measure:
- Switching time
- Purge volume
- Color-contamination risk
- Coating waste
- Labor time
- First acceptable part time
Compare:
- Machine investment
- Installation cost
- Coating consumption
- Cleaning material cost
- Labor cost
- Maintenance cost
- Spare-part cost
- Downtime cost
- Expected production output
Expert insight: Do not compare only the purchase price. A dual-circuit system may cost more initially but deliver a lower total cost when frequent color changes reduce throughput in a single-circuit line.
Film build is the thickness of coating applied to the workpiece. It affects appearance, durability, drying time, and downstream sanding.
In both systems, film build is influenced by:
- Fluid output
- Spray-gun settings
- Atomizing air
- Fan air
- Gun distance
- Line speed
- Coating viscosity
- Number of passes
A dual-circuit system can help maintain consistent film build when each circuit is dedicated to a specific coating or viscosity range.
Color consistency depends on:
- Coating mixing accuracy
- Viscosity control
- Clean fluid lines
- Stable pump delivery
- Correct gun settings
- Clean spray guns and nozzles
- Consistent substrate color
- Proper flushing between colors
A dual-circuit system can reduce cross-contamination when circuits are properly isolated. However, poor valve sealing, worn hoses, or inadequate cleaning can still cause color defects.
Color contamination may appear as:
- Tinted streaks
- Cloudy clear coat
- Inconsistent color between parts
- Dark or light spots
- Poor hiding power
- Uneven gloss
Likely causes:
- Incomplete flushing
- Worn valves or seals
- Coating left in hoses
- Incorrect purge procedure
- Incompatible coatings
- Contaminated filters
- Poor coating preparation
Solution: Standardize the flushing sequence, inspect valves and seals, verify coating compatibility, and run a controlled purge before releasing production parts.
Both single-circuit and dual-circuit systems can handle:
- Water-based primers and topcoats
- Solvent-based lacquers
- UV-curable coatings
- Stains and glazes
- Sealers
- Protective clear coats
Each coating has different viscosity, drying behavior, cleaning requirements, and material compatibility.
Water-based coatings often require controlled temperature and airflow during drying. They are generally easier to clean up, but equipment compatibility must still be verified.
Solvent-based coatings may flash off faster depending on the formulation. They require compatible hoses, seals, pumps, and solvent-based cleaning procedures.
Important: "Water-based" does not mean "no ventilation required." OSHA notes that the need for spray booth ventilation depends on the presence of hazardous chemicals in the coating, not simply whether the coating is water-based. [1805]
Spray finishing can release mists, vapors, and residues. OSHA identifies spray finishing using flammable and combustible liquids as a regulated operation under 29 CFR 1910.107. [1720]
A spray booth is a power-ventilated structure provided to enclose or accommodate a spraying operation, confine and limit the escape of spray, vapor, and residue, and safely direct them to an exhaust system. [1720]
OSHA requires mechanical ventilation in spraying areas to remove flammable vapors, mists, or powders to a safe location and to confine and control combustible residues. [1720]
Ventilation must remain in operation during spraying and for a sufficient time afterward to allow vapors from drying coated articles and finishing-material residue to be exhausted. [1720]
OSHA also states that the total air volume exhausted through a spray booth should dilute solvent vapor to at least 25 percent of the lower explosive limit of the solvent being sprayed. [2202]
Both single-circuit and dual-circuit systems should include:
- Properly designed spray booth or enclosed spray zone
- Mechanical exhaust ventilation
- Make-up air supply
- Filter maintenance program
- Grounding and bonding for static control
- Appropriate electrical classification where required
- Coating storage and handling controls
- Operator training
- Emergency stop and interlock systems
- Regular inspection of hoses, pumps, valves, guns, and filters
Do not treat ventilation as an optional accessory. It is a core safety and quality system.
- You run long batches of one color.
- Color changes are infrequent.
- You need a compact, lower-complexity system.
- You want lower initial investment.
- Your operators can manage a standardized flushing process.
- Coating waste during changeover is acceptable.
- You change between two colors frequently.
- You need to reduce line downtime.
- You use two coatings with different viscosities or functions.
- You want to separate primer and topcoat supply.
- You produce short batches with predictable color pairs.
- You need to reduce full-system flushing frequency.
- You use more than two colors frequently.
- You need rapid switching among several coatings.
- You have high-mix, low-volume production.
- You need to reduce manual touch-up and color contamination.
- You want to future-proof the line for changing product mixes.
A modular multi-circuit approach may cost more initially, but it can be justified when color changes are a major constraint on output.
Document the colors, coatings, batch sizes, change frequency, and quality standard.
Include the two most frequent color pairs and the most difficult coating transition.
Test the actual product with the intended coating. Record:
- Coating viscosity
- Fluid output
- Spray-gun settings
- Atomizing air
- Fan air
- Line speed
- Number of passes
- Film thickness
- Drying result
- Color consistency
- Visual appearance
Do not judge only the spray station. Validate the complete sequence:
Coating → flash-off → cure → sanding if required → second coat if required → final inspection.
Operators should understand daily checks, coating preparation, color-change procedures, and quality inspection. Technicians should understand pump setup, valve operation, filters, hoses, electrical controls, and safety systems.
Create written recipes for each color and coating. Include viscosity, gun settings, line speed, curing conditions, and inspection criteria.
Schedule maintenance for filters, nozzles, pumps, hoses, valves, conveyors, sensors, and ventilation equipment.
Likely causes:
- Incomplete flushing
- Worn valves or seals
- Coating left in hoses
- Incorrect purge procedure
- Incompatible coatings
- Contaminated filters
Solution: Standardize the flushing sequence, inspect valves and seals, verify coating compatibility, and run a controlled purge before releasing production parts.
Likely causes:
- Air in the coating supply
- Worn pump components
- Blocked filters
- Incorrect viscosity
- Hose restriction
- Valve leakage
Solution: Check the coating supply, filter condition, pump performance, and valve operation. Adjust one variable at a time and document the result.
Likely causes:
- Inconsistent coating mixing
- Changes in viscosity
- Different gun settings
- Inconsistent substrate color
- Inadequate cleaning between color changes
Solution: Standardize mixing, viscosity checks, gun recipes, and cleaning procedures.
Likely causes:
- Long fluid lines
- Excessive purge volume
- Inefficient cleaning sequence
- Frequent unnecessary color changes
- Poor production scheduling
Solution: Reduce hose length where possible, optimize purge volume, group similar colors, and schedule color changes strategically.
Likely causes:
- Manual flushing steps
- Missing spare parts
- Unclear procedures
- Inadequate operator training
- Poor production planning
Solution: Create a written standard operating procedure, train operators, keep critical spares available, and measure changeover time continuously.
- Inspect spray guns and nozzles.
- Check fluid hoses and connections.
- Confirm conveyor alignment.
- Verify booth airflow and filter condition.
- Inspect pumps, valves, and fluid lines.
- Check for leaks, air bubbles, or pressure fluctuation.
- Clean gun tips according to the coating manufacturer's instructions.
- Inspect emergency stops and safety interlocks.
- Check belt tension and conveyor tracking.
- Inspect gun carriage movement.
- Clean or replace filters as required.
- Check pump performance and fluid delivery.
- Inspect valve sealing and circuit isolation.
- Review coating consumption and reject rates.
- Inspect ventilation fans and ducts.
- Check electrical connections and control panels.
- Review PLC alarms and error history.
- Calibrate sensors and verify safety devices.
- Audit recipes against actual production results.
GYDFinishing has manufactured surface finishing equipment since 2007 and provides solutions for wood, glass, fibre cement, and other materials. Its experience includes automatic coating equipment for wooden doors, furniture, cabinet doors, and flooring.
For a buyer comparing a single-circuit spray system with a dual-circuit spray system, the most useful supplier discussion is not simply about machine type. It should focus on:
- The exact product mix and color-change frequency
- Coating types and target film thickness
- Required production output
- Available factory space and utilities
- Curing method and drying time
- Color-change procedure
- Operator skill level
- Maintenance and spare-part strategy
- Total cost of ownership
A credible supplier should be willing to test the customer's actual coatings and color-change workflow, document the results, and explain the limitations as well as the benefits.
A single-circuit system uses one coating supply path for all colors. A dual-circuit system uses two independent coating paths, allowing faster switching between two colors or coatings.
A dual-circuit system is usually better when production regularly alternates between two colors or coatings. It can reduce full-system flushing and downtime.
Yes, provided the machine, pump, hoses, valves, nozzles, and drying system are compatible with the coating. Water-based coatings still require proper ventilation when hazardous chemicals are present. [1805]
No. Both circuits still require cleaning and maintenance. A dual-circuit system reduces the frequency of full-system flushing but does not eliminate coating-change procedures.
Compare the cost of current color-change downtime, coating waste, cleaning materials, and labor against the additional investment, maintenance, and operating cost of a dual-circuit system.
Yes. Multi-circuit or modular systems can support more than two colors or coatings. They are useful for high-mix production but require more complex controls, cleaning, and maintenance.
If you are deciding between a single-circuit and dual-circuit spray system for frequent color changes, start with a color-change workflow audit rather than a generic equipment quotation.
Send GYDFinishing your color-change frequency, coating specification, target output, and factory layout. A practical evaluation should identify the right circuit configuration, flushing procedure, curing method, and total line layout for your product family.
- After the introduction: AI image prompt: *Side-by-side industrial comparison of a single-circuit and dual-circuit spray system coating wooden door panels, clean modern factory, realistic photography, wide angle.*
- In the "How Each System Works" section: AI image prompt: *Cutaway technical illustration comparing a single-circuit spray system and a dual-circuit spray system with two coating supply paths, pumps, valves, and spray guns, clean engineering illustration.*
- In the "Color-Change Downtime" section: AI image prompt: *Factory workflow illustration showing color change steps: line stop, flushing, refilling, testing, and production restart, no text.*
- In the "Ventilation" section: AI image prompt: *Technical illustration of spray booth airflow, intake air, exhaust duct, filters, and wooden panels moving through the booth.*
- In the "Validation Roadmap" section: AI image prompt: *Flowchart-style factory illustration showing coating supply, spray application, flash-off, curing, inspection, and packaging.*
- OSHA, *29 CFR 1910.107 – Spray finishing using flammable and combustible materials*: [https://www.osha.gov/laws-regs/regulations/standardnumber/1910/1910.107]
- OSHA, *29 CFR 1910.94 – Ventilation*: [https://www.osha.gov/laws-regs/regulations/standardnumber/1910/1910.94]
- OSHA, *Spray Operations – Overview*: [https://www.osha.gov/spray-operations]
- OSHA, *Spray Operations – Controlling Hazards*: [https://www.osha.gov/spray-operations/controlling-hazards]
- OSHA, *Spray Operations – Standards*: [https://www.osha.gov/spray-operations/standards]
- OSHA, *The airflow rate required for a spray painting area*: [https://www.osha.gov/laws-regs/standardinterpretations/1997-04-08-0]
- OSHA, *Requirements for spray booth when spraying water-based paint*: [https://www.osha.gov/laws-regs/standardinterpretations/2008-03-28]
- OSHA, *Clarification Paint Spray Booth and Spray Areas*: [https://www.osha.gov/laws-regs/standardinterpretations/1976-11-04]
- GYDFinishing company background supplied by the client.


